
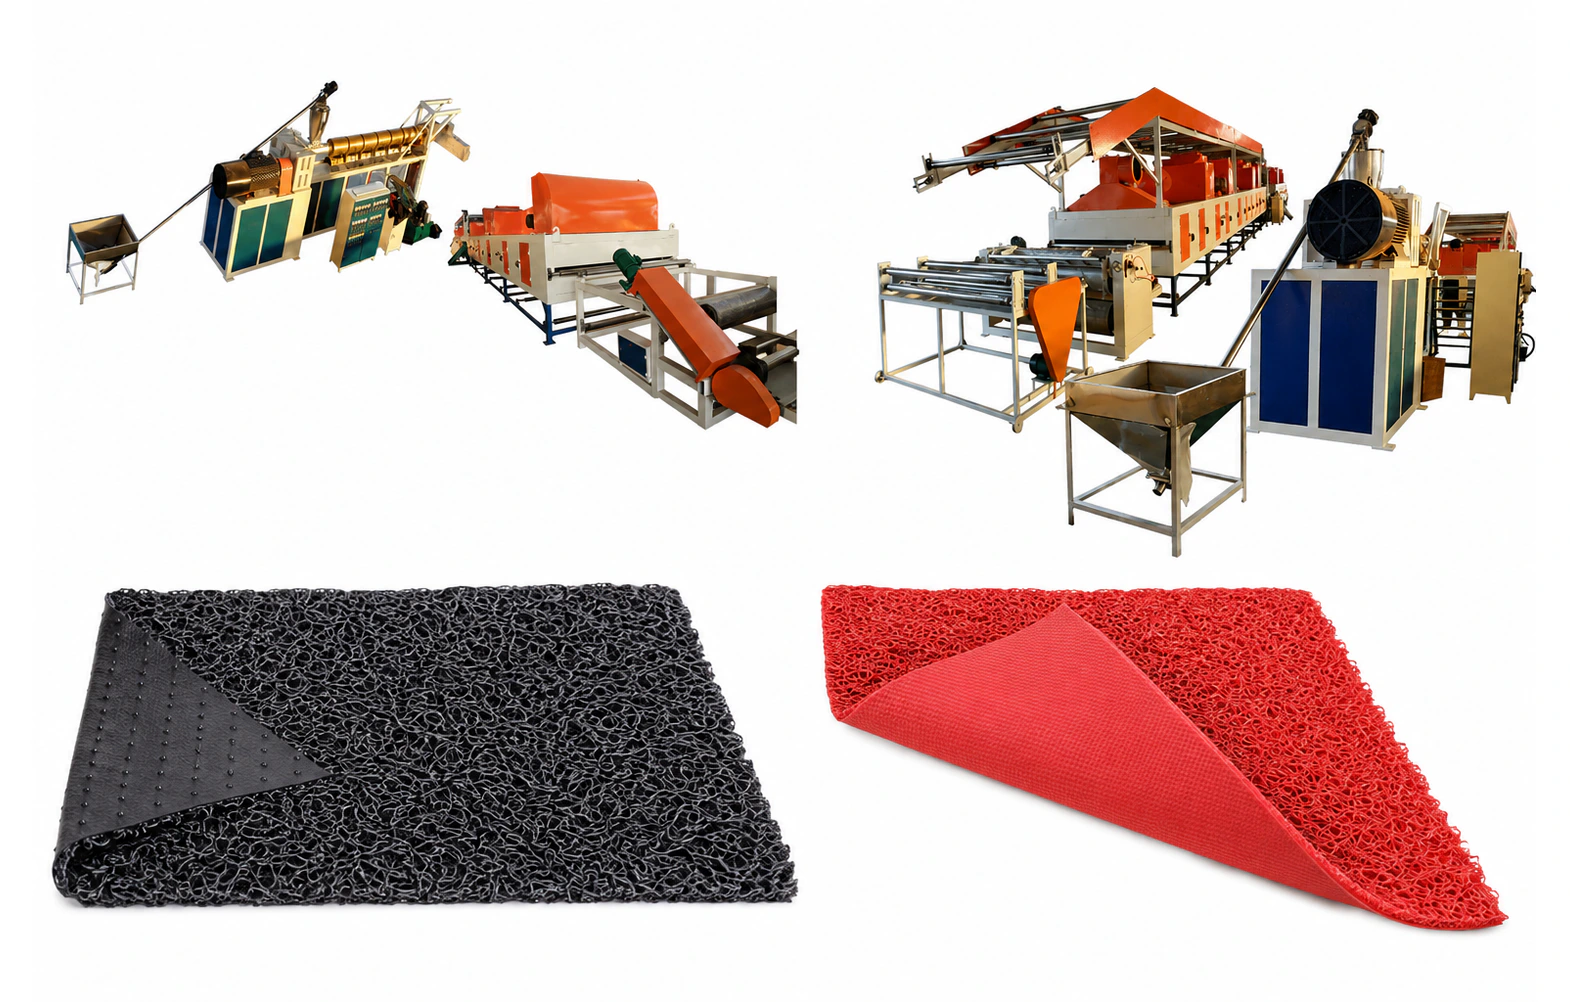
PVC Coil Loop Car & Door Mat Extrusion Machine
Product Overview
The PVC Coil Loop Car & Door Mat Extrusion Machine covers two closely related tangled-loop products: coil-loop automotive mats and coil-loop entrance mats with PVC foam backing. Both use dedicated loop extrusion and thermal forming, while the downstream backing route is configured separately for the required finished product.
A car-mat configuration uses one or two color extruders, a loop-forming die, controlled heating, a forming-water section, cooling, and either stacking or online backing integration. Automotive products can use spike or diamond-style backing and are subsequently cut to vehicle-specific shapes.
For foam-backed entrance or door mats, the loop layer proceeds through heating/oven stages and is joined with an expanded PVC backing through the specified bonding and calendering route before trimming and winding. This page does not represent chain-link, coin-pattern, S-shaped, puzzle, or sheet-flooring products.
Typical published configurations are designed around a 1200 mm working width and output up to approximately 500 kg/h. Final performance depends on loop height, density, color count, backing weight, oven duty, and line speed.
Key Features
Dedicated tangled-loop extrusion and controlled loop-forming system
Single-color or two-color automotive coil-loop configurations
Separate foam-backing, oven, calendering, and bonding route for door mats
Configurable spike, diamond, or expanded-PVC backing construction
Automatic stacking or trimming and winding matched to the finished format
Production Process
The process route is configured around the finished mat structure, backing, width, and output target.
Compound & Color Preparation
Flexible PVC compound and pigment are prepared for the required loop elasticity, color, weather resistance, and odor target.
Loop Extrusion
One or two loop extruders feed the dedicated die to form continuous PVC filaments at a controlled melt rate.
Heating & Loop Forming
Infrared heating and the forming-water section set the tangled-loop height, density, openness, and surface recovery.
Cooling & Structure Stabilization
Controlled cooling stabilizes the loop layer before it enters the selected automotive or entrance-mat backing route.
Backing Integration
Automotive mats receive the specified spike or diamond backing; door mats receive a PVC foam backing through heating, bonding, and calendering stages.
Stacking, Trimming or Winding
The product is stacked, edge-trimmed, cut, or wound according to the intended car-mat blank or entrance-mat roll format.
Technical Specifications
| Finished Products | Coil-loop automotive mats; PVC foam-backed coil-loop entrance/door mats |
|---|---|
| Typical Working Width | Approximately 1200 mm |
| Nominal Output | Up to approximately 500 kg/h, configuration dependent |
| Single-Color Example | One 120/30 loop extruder plus one 120/30 backing extruder |
| Two-Color Example | Two 100/30 loop extruders plus one 120/30 backing extruder |
| Installed Power | Approximately 300 kW for a complete configured line |
Configuration Guidance
Choose the Product Route
Confirm automotive mat or foam-backed entrance mat first; they share loop extrusion but use different backing and finishing modules.
Define Loop Geometry
Provide loop height, density, filament color, surface openness, and sample photographs so the die and forming settings match the product.
Specify the Backing
Spike, diamond, or expanded-PVC foam backing changes extruder count, oven duty, bonding, cooling, and winding requirements.
Confirm Final Format
Vehicle blanks, stacked sheets, entrance-mat rolls, and cut mats require different trimming, stacking, cutting, or winding layouts.
Quality Checks
- Measure loop height, density, weight per square meter, elasticity, and color consistency.
- Check the loop layer for bare areas, collapsed coils, overheating, or uneven cooling.
- Verify backing thickness, spike or foam pattern, peel strength, and full-width bond consistency.
- Confirm edge trim, stack alignment, winding tension, and finished roll dimensions.
Typical Applications
Frequently Asked Questions
They share the dedicated PVC coil-loop extrusion and forming principle. The backing, oven, bonding, and finishing sections are then configured separately for automotive or entrance-mat production.
No. Chain and coin mats belong to the calender product family and use the separate PVC Calender Anti-Slip Chain & Coin Mat Extrusion Machine.
Yes. A typical two-color configuration uses two 100/30 loop extruders with one 120/30 backing extruder; the final selection depends on output and compound.
Provide the finished width, loop height and density, color count, backing type and thickness, output target, final roll or blank size, voltage, and available factory layout.
Related Products
Related Technical Articles
Plan Your Coil Loop Mat Line
Send a finished-mat sample or clear photos plus width, loop height, density, colors, backing structure, output, and final format. We will separate the correct extrusion, forming, backing, and finishing modules.
Contact Us