
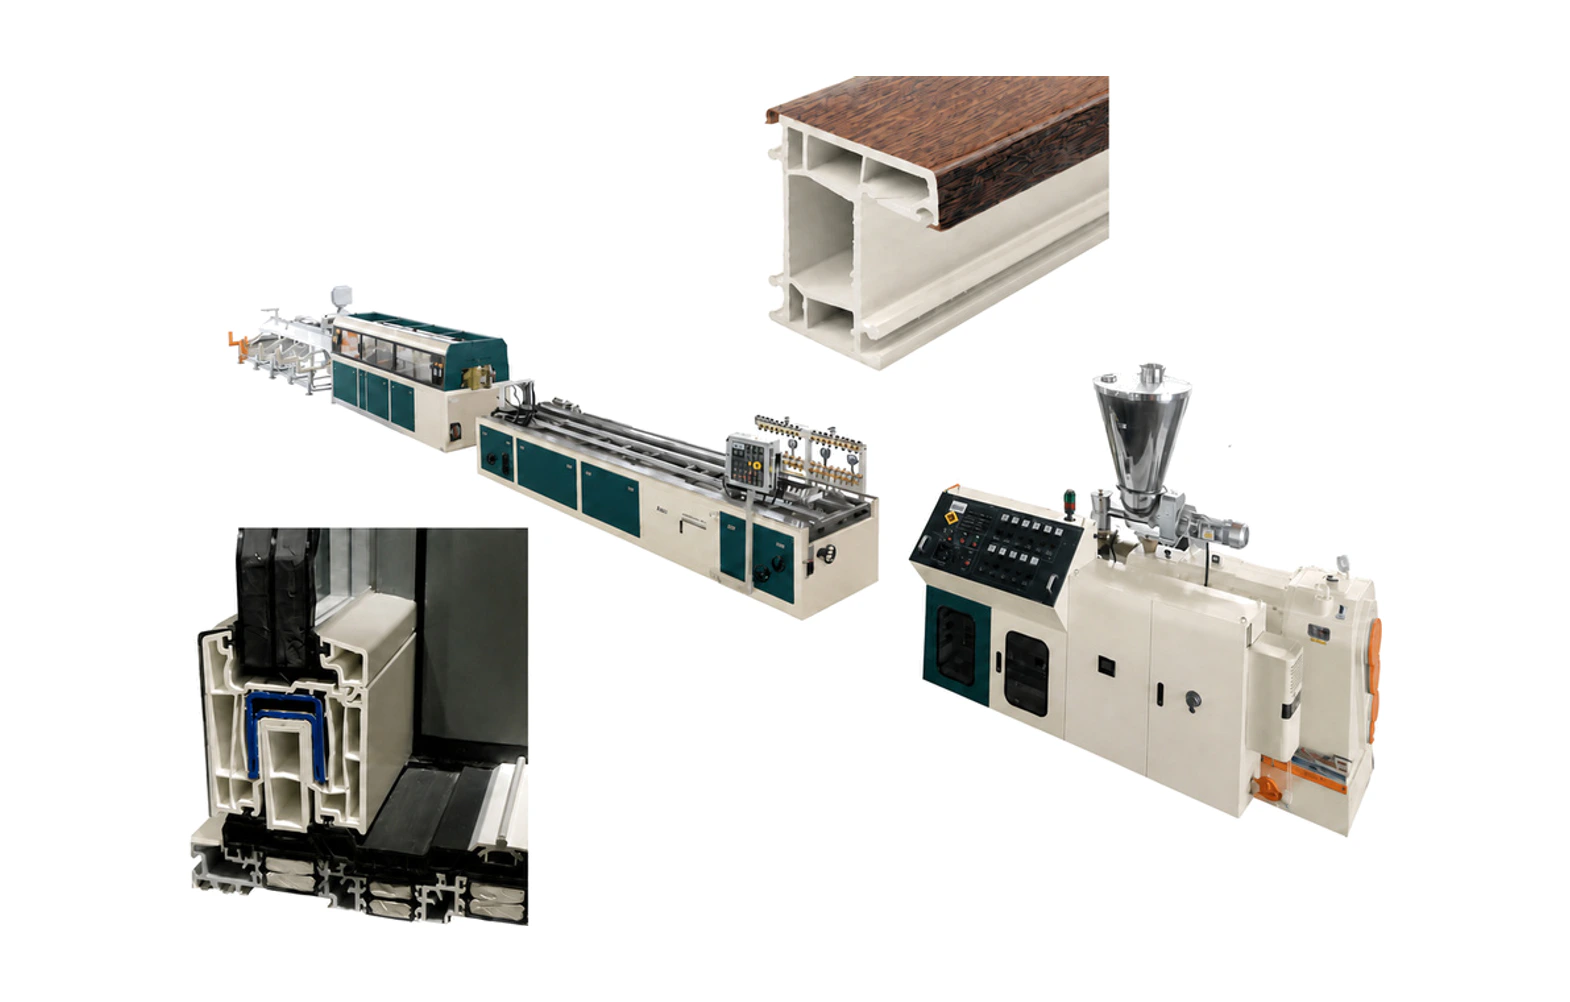
PVC Window Profile Extrusion Line
Product Overview
The PVC Window Profile Extrusion Line is a high-precision production system designed for manufacturing multi-chamber PVC window and door profiles. These profiles are the structural backbone of modern vinyl windows, requiring exceptional dimensional accuracy, surface quality, and mechanical strength to meet international window performance standards.
Our line is built around an SJSZ-80/156 or SJSZ-92/188 conical twin-screw extruder, paired with a multi-cavity die, an extended vacuum calibration table (6m+), and dual haul-off system. It supports 60, 80, and 88 series profiles for both casement and sliding window applications, with optional steel reinforcement co-extrusion for enhanced structural rigidity.
Window profile extrusion demands the highest precision in the PVC profile category. Wall thickness tolerances must be controlled within ±0.1mm, surface must be free of flow marks and color variation, and the profile must maintain straightness over long lengths. Our die design uses computational fluid dynamics (CFD) simulation to optimize flow channels, ensuring uniform material distribution and minimizing internal stress.
The production line includes steel reinforcement co-extrusion capability, allowing galvanized steel profiles to be integrated into the PVC profile during extrusion. This feature is critical for large window frames and structural applications where additional rigidity is required by building codes.
Key Features
High-precision conical twin-screw extruder
Multi-cavity die design for window profiles
Steel reinforcement co-extrusion unit
Long vacuum calibration table (6m+)
Dual haul-off and cutting system
Production Process
From raw material to finished product — each step is engineered for quality and efficiency.
Formulation & Mixing
Lead-free Ca-Zn stabilized formulation with high-grade TiO2 (4-6 parts) for UV protection, CPE impact modifier (8-10 parts), and process aids. Mixed at 125°C in high-speed mixer.
Extrusion & Homogenization
The compound is plasticized in the conical twin-screw extruder at 170-195°C. Precise zone temperature control ensures complete gelation without degradation.
Multi-Cavity Die Forming
The molten PVC flows through a precision multi-cavity die that creates the complex window profile cross-section with internal chambers, grooves for hardware, and steel reinforcement channels.
Vacuum Calibration & Cooling
The profile enters a long vacuum calibrator (6-8 meters) with multiple cooling zones. Precise vacuum levels and water temperature control ensure dimensional stability and surface quality.
Steel Co-Extrusion (Optional)
For reinforced profiles, galvanized steel strips are fed into the profile channels during extrusion, creating a composite PVC-steel structure for structural applications.
Haul-off, Cutting & Storage
Dual caterpillar haul-off ensures smooth, mark-free pulling. A precision saw cuts profiles to 6m standard length. Profiles are stored on specialized racks to prevent deformation.
Technical Specifications
| Extruder Model | SJSZ-80/156 or SJSZ-92/188 |
|---|---|
| Profile Series | 60 / 80 / 88 series |
| Profile Type | Casement / Sliding |
| Production Speed | 2-4 m/min |
| Total Power | ~110-160 kW |
| Line Length | ~30m |
Why Choose Wings Plastic
CFD-Optimized Die Design
Our dies are designed using computational fluid dynamics simulation to balance flow distribution across complex multi-cavity profiles, eliminating weld lines and thickness variations.
Extended Calibration Table
A 6-8 meter vacuum calibration table with independent zone control provides superior cooling and dimensional stability — critical for window profiles that must meet stringent tolerance requirements.
Steel Co-Extrusion Ready
Integrated steel reinforcement feeding system enables production of structural window profiles meeting European and American building code requirements for large-span windows.
High TiO2 Formulation
Line is configured for high-TiO2 formulations (4-6 parts) ensuring excellent UV resistance and weatherability for profiles exposed to direct sunlight for 20+ years.
Dual Haul-off System
Dual caterpillar haul-off with soft pads prevents surface marking on high-gloss profiles, maintaining the premium surface quality required for visible window applications.
Quality Assurance
Every production line undergoes rigorous quality verification before delivery:
- Wall thickness measured at 8 points around the profile cross-section using digital gauges
- Surface quality inspected for gloss uniformity, flow marks, and color matching against standards
- Welding strength tested per EN 514 to ensure corner joint integrity after window fabrication
- Accelerated weathering test (QUV) verifies UV stability and color retention over simulated 10-year exposure
Typical Applications
Frequently Asked Questions
The line supports 60 series (residential casement), 80 series (sliding windows), and 88 series (large sliding doors). Die sets for each series are interchangeable on the same extruder.
A complete die and calibrator change takes 3-4 hours, including die heating, calibration adjustment, and line tuning. We recommend scheduling changeovers during planned maintenance windows.
Yes, profiles produced on this line can meet EN 12608 Class A or B requirements when using appropriate formulations. We provide formulation guidance and certification support for European markets.
This optional system feeds galvanized steel profiles into the PVC profile chambers during extrusion. It is recommended for profiles longer than 1.5m or where building codes require steel-reinforced vinyl window frames.
Related Products
Related Technical Articles
Ready to Get Started?
Contact our team for a customized PVC Window Profile Extrusion Line solution tailored to your production needs.
Contact Us